Roux Lab operates as a specialized supply chain catalyst, securing seamless delivery of critical raw materials, active pharmaceutical ingredients, high-purity filtration systems, and rigorous QC laboratory essentials with full regulatory traceability.
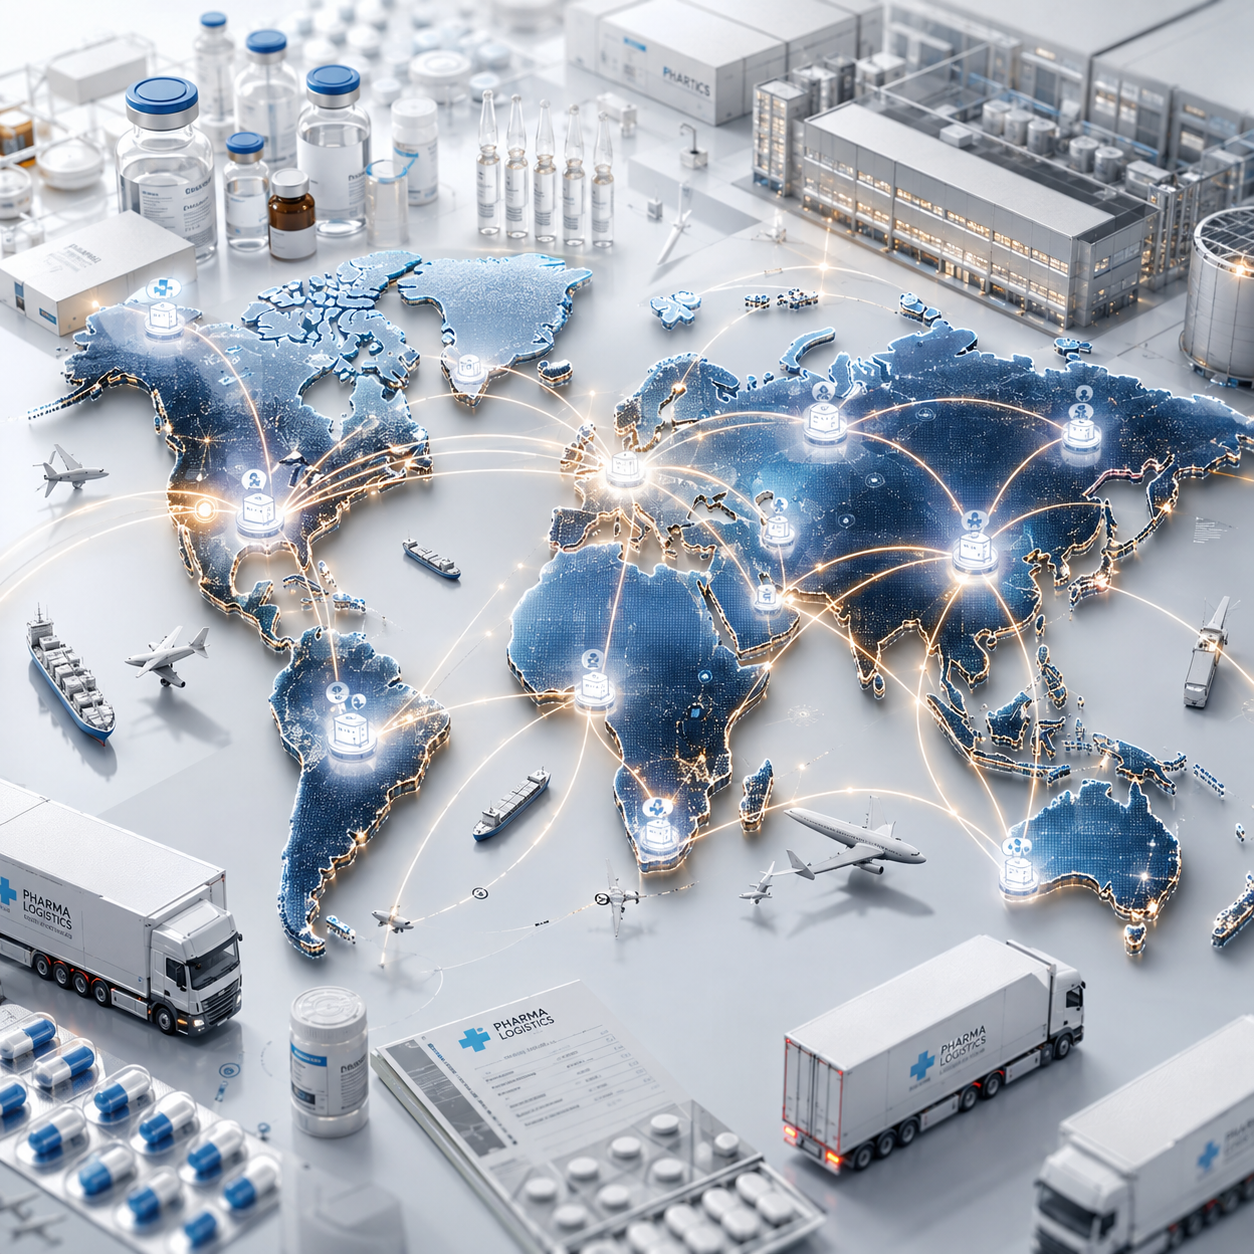
Direct channels to audited tier-1 production facilities worldwide.
We eliminate supply chain friction and protect your production continuity through rigorous compliance.
Every delivery is accompanied by verified Certificates of Analysis (CoA) and Certificates of Conformance (CoC) to meet stringent audit criteria.
Custom inventory management and forecasting frameworks designed to buffer your facility against unexpected global logistics bottlenecks.
Full support for change control notifications, USP/EP pharmacopoeia compliance documents, and material safety data evaluations.
Sourcing high-grade materials and equipment across seven critical pharmaceutical pillars.
Sterile-grade membrane discs, syringe filters (PES, PTFE, PVDF, Nylon), capsule filters, and single-use fluid transfer assemblies.
HPLC/GC systems, dissolution testers, spectrophotometers, analytical balances, moisture analyzers, and cleanroom monitoring devices.
Sourcing and verification of high-purity Active Pharmaceutical Ingredients (APIs), specialized excipients, and regulatory dossier support.
ACS/HPLC grade solvents, pharmacopoeia reference standards (USP/EP), analytical buffers, and custom synthesis reagents.
Bacterial Endotoxin Test (BET) kits, LAL reagents, ELISA kits for biological quantification, and diagnostic validation standards.
Borosilicate glassware, low-retention tips, certified HPLC vials, sterile garments, lint-free wipes, and gamma-irradiated nitrile gloves.
At Roux Lab, we understand that manufacturing integrity depends on raw material purity. Our supply chain partners undergo rigorous audit protocols to guarantee compliance with international pharmacopoeias.
Submit your technical specifications or upload your Bill of Materials (BOM) file for prompt processing.